Precision Coil Slitting Solution
1850 High Precision Slitting Line with Belt Tension System
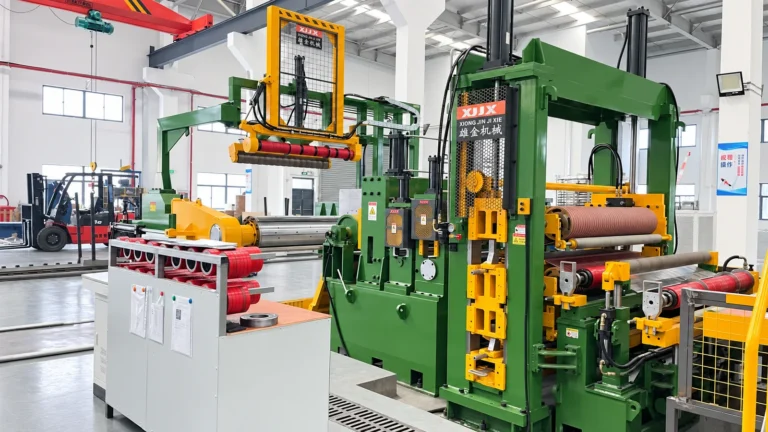
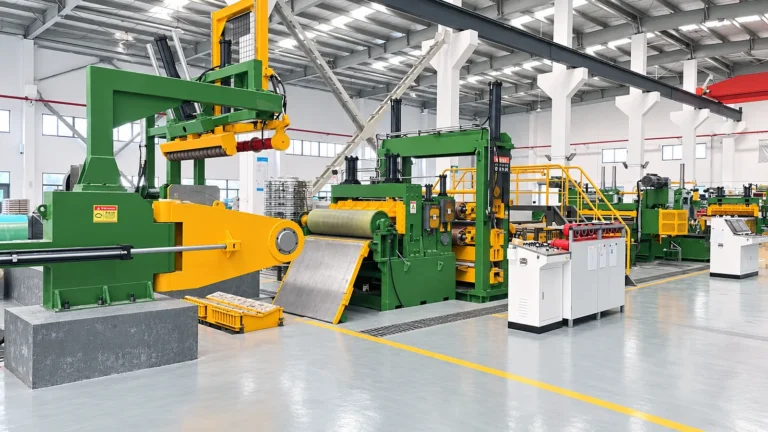
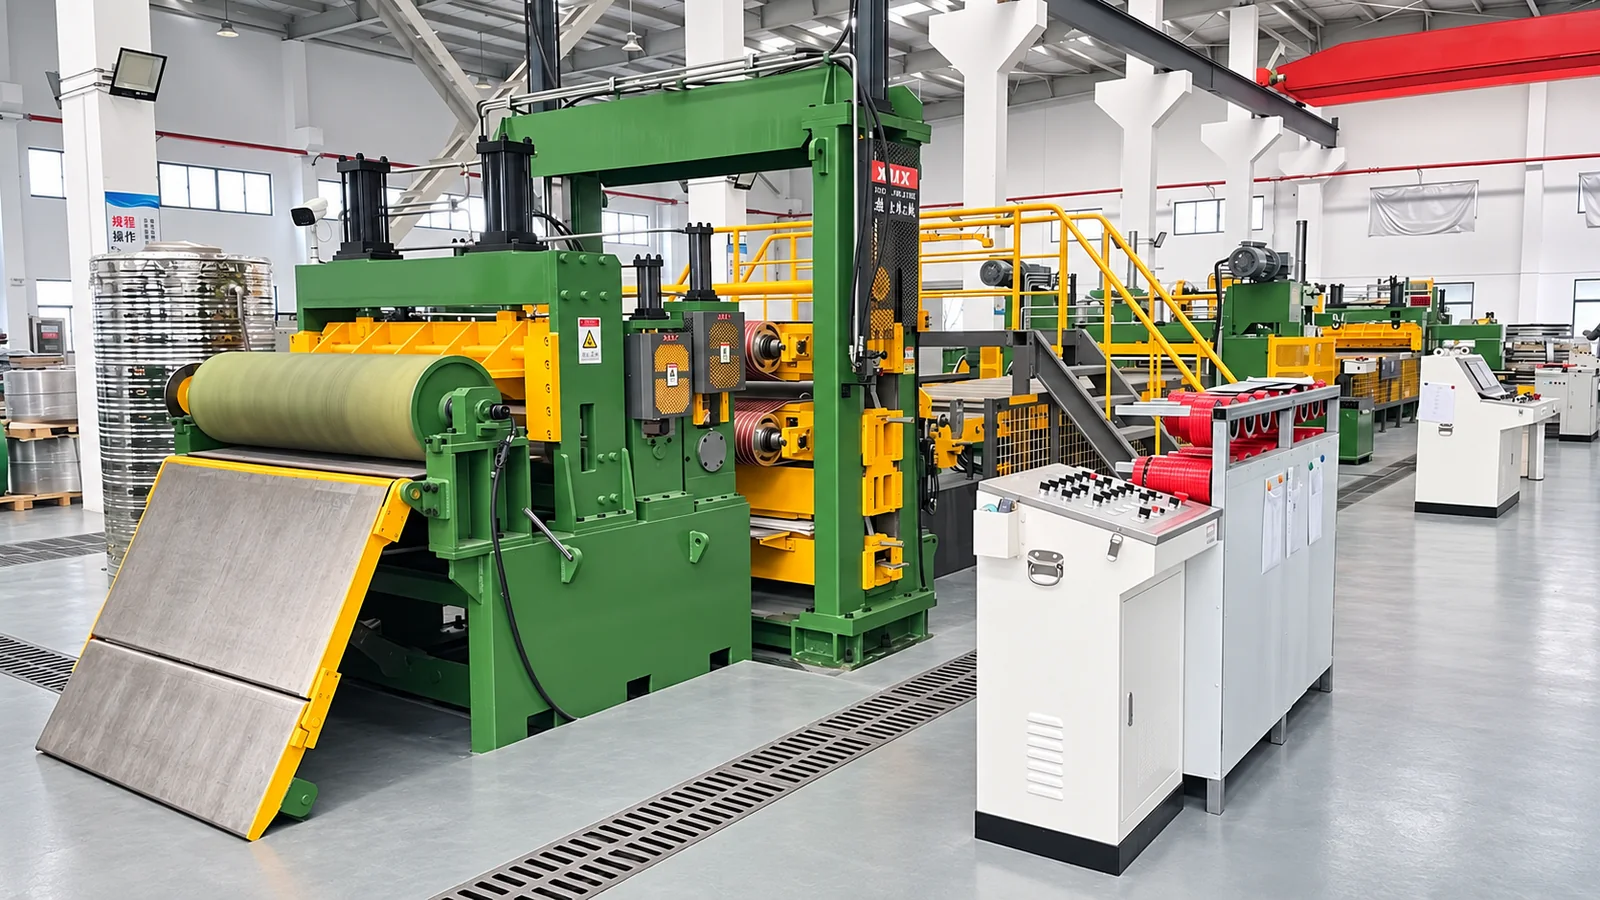
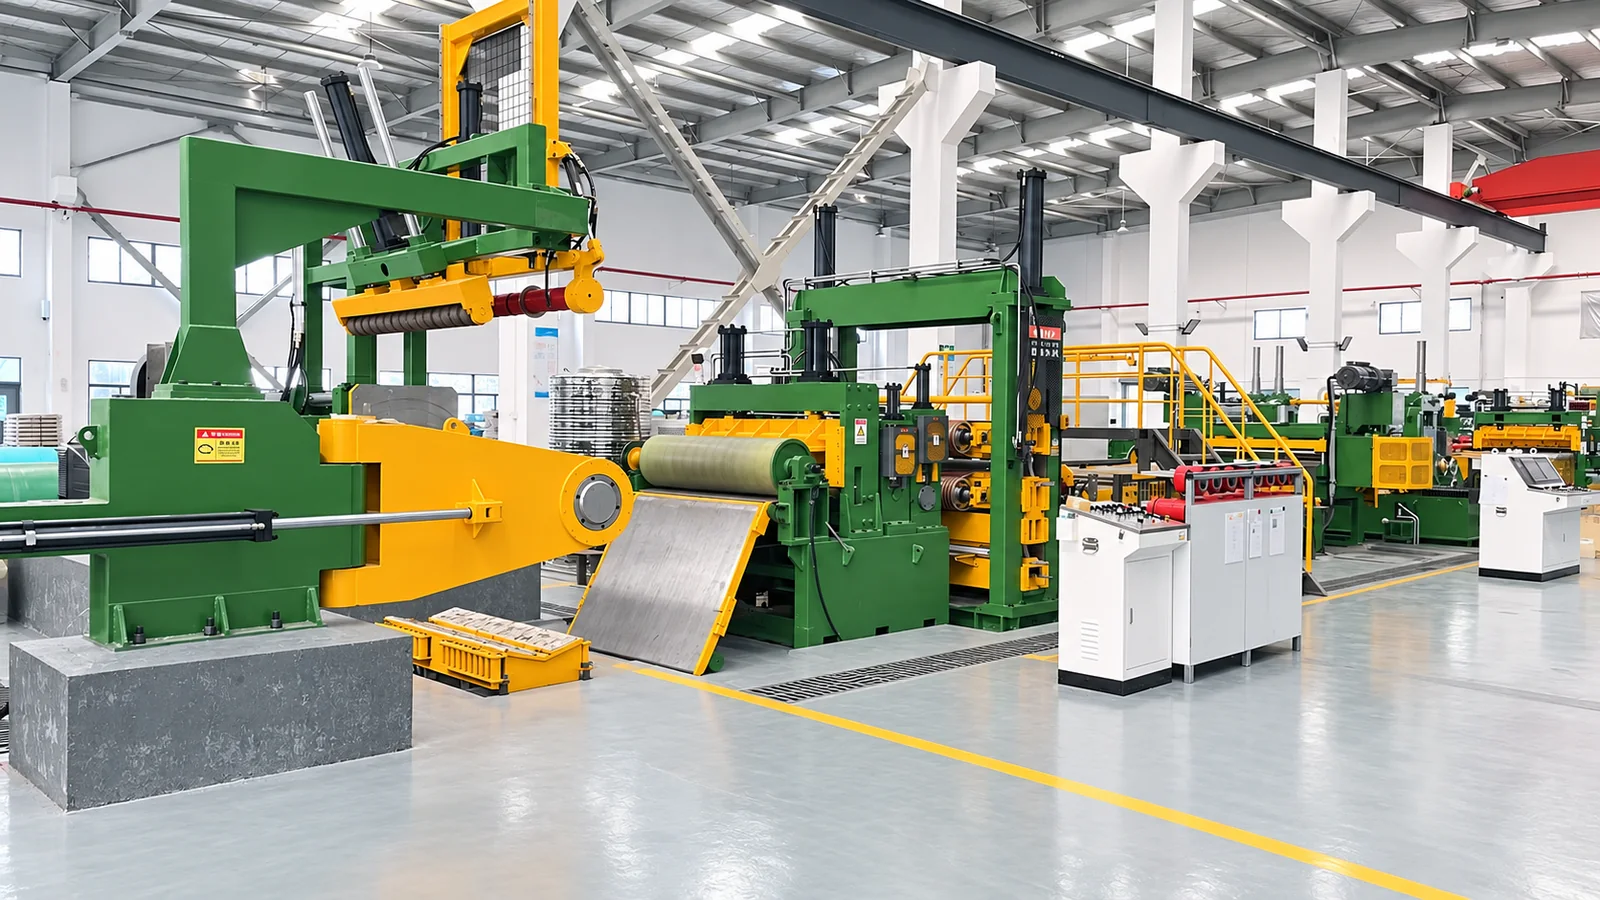
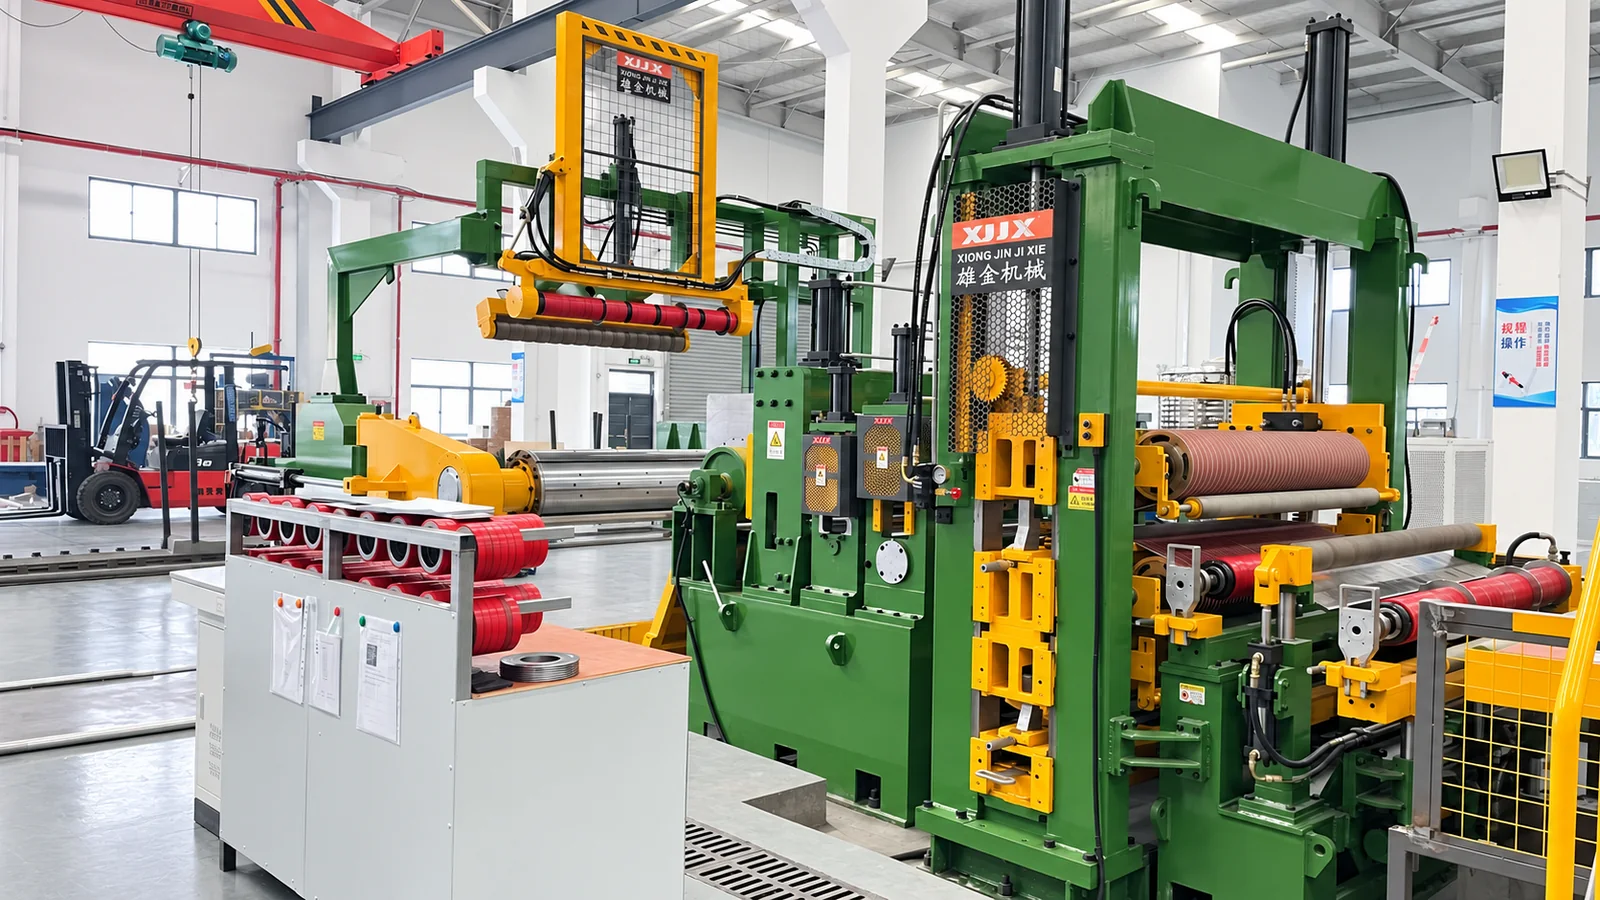
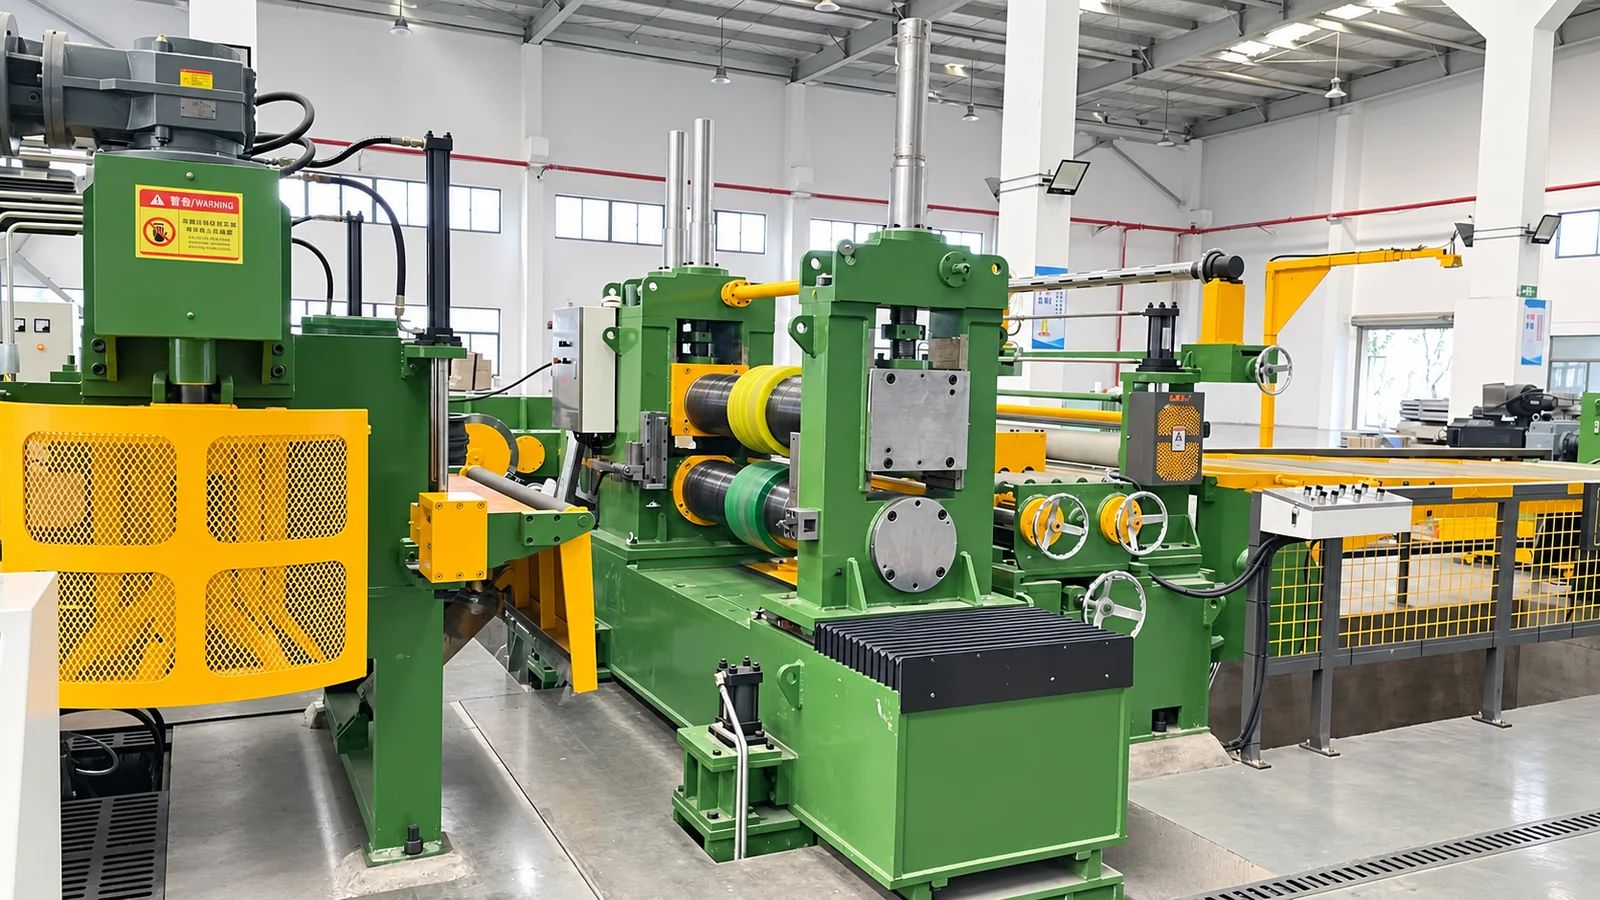
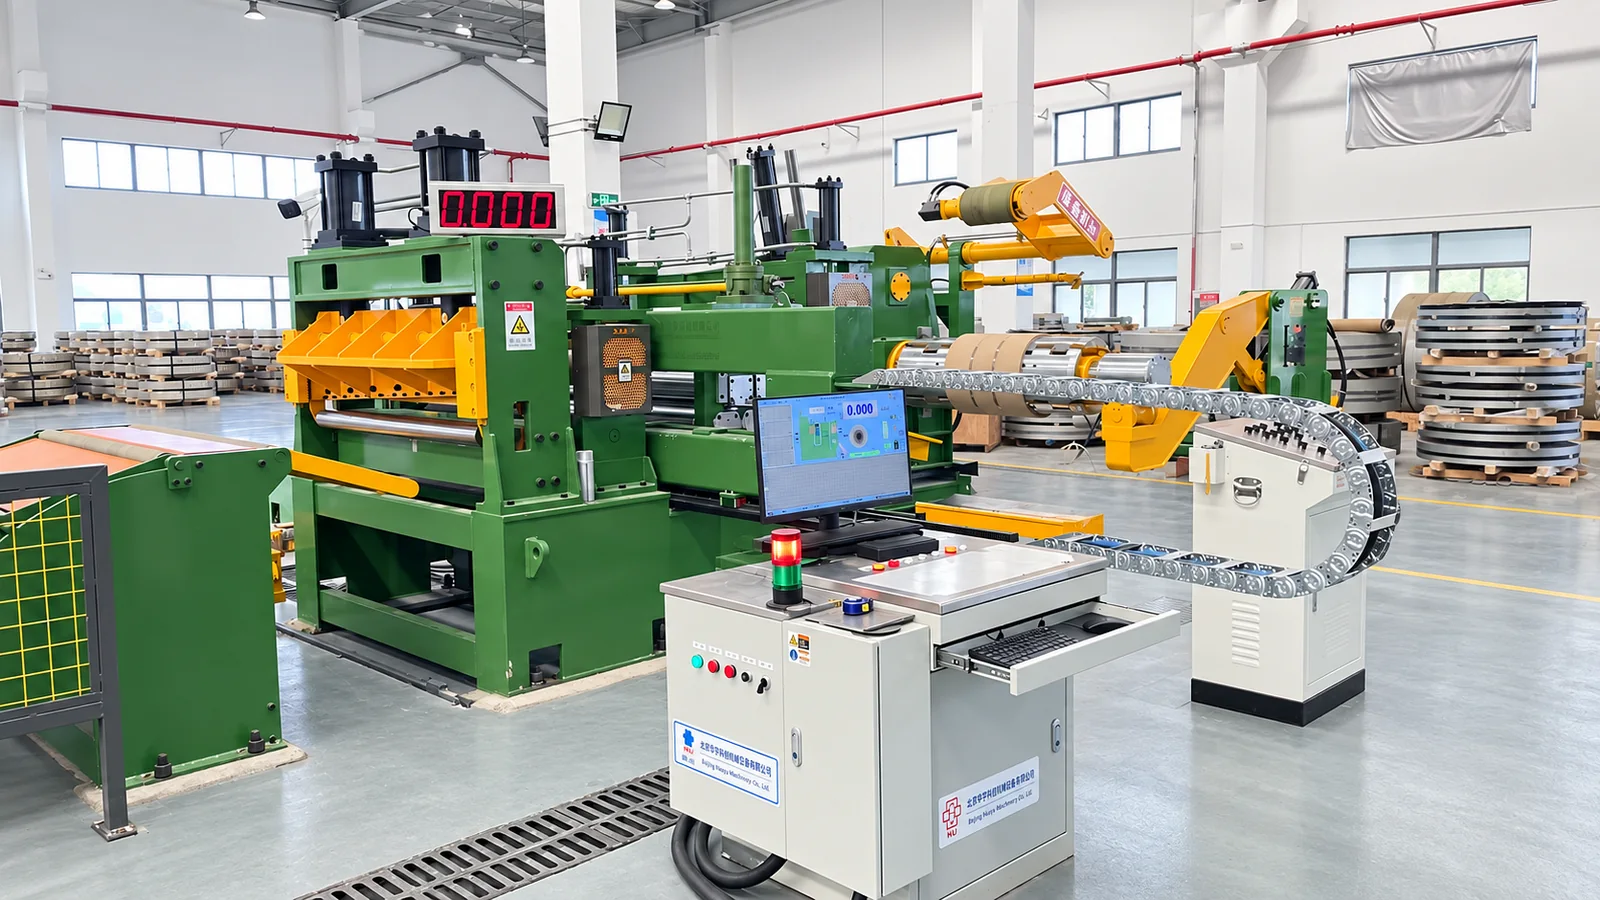
XIONGJIN’s 1850 High Precision Slitting Line with Belt Tension System is engineered for controlled conversion of wide metal coils into accurately slit strips. The line combines stable coil handling, precision slitting, belt-based strip-tension control and orderly recoiling to support consistent coil build and surface-conscious processing.
The 1850-type configuration is designed for galvanized steel, stainless-steel and pre-painted/color-coated coil applications with a maximum coil width of 1800 mm. The final line arrangement is matched to the customer’s material grade, thickness, slit pattern, tolerance target and production requirement. As part of our thin gauge slitting line series, this belt-tension model complements the 1350 High Precision Slitting Line and the 1650 Thin-Gauge Slitting Line — see the 1850 belt tensioner slitting line installation for field results.
The figures below are reference technical parameters for this configuration. XIONGJIN confirms the final scope, auxiliary equipment and acceptance method against the customer’s actual coil data and process requirements.
Raw Material Technical Parameters
| Applicable Coil Materials | Galvanized steel coil, stainless-steel coil and pre-painted/color-coated steel coil |
|---|---|
| Material Thickness | 0.3–4.0 mm |
| Maximum Coil Width | 1800 mm |
| Maximum Coil Outside Diameter | ≤ 1800 mm |
| Coil Inside Diameter | 508 mm |
| Maximum Coil Weight | 25 MT |
| Reference Material Strength | Tensile strength σb ≤ 510 MPa |
Finished Strip and Coil Parameters
| Finished Coil Inside Diameter | 508 mm |
|---|---|
| Finished Coil Outside Diameter | ≤ 1800 mm |
| Maximum Finished Coil Weight | 25 MT |
| Reference Number of Strips | Up to 40 strips at 0.5 mm; up to 10 strips at 4.0 mm, depending on slit pattern and material |
| Minimum Finished Strip Width | 15 mm |
| Scrap Edge Width Range | 2–15 mm |
| Strip Width Tolerance | ≤ ±0.05 mm |
| Burr | ≤ 0.03 mm |
| Reference Straightness | ≤ 0.8 mm/m for slit widths ≤ 30 mm; ≤ 0.5 mm/m for slit widths > 30 mm. The first and last 10 m are excluded. |
Typical Line Configuration
- Coil Loading Car: transfers the master coil safely onto the uncoiler centreline.
- Hydraulic Uncoiler with Support Arm: provides stable, controlled pay-off for coils up to the configured weight.
- Coil Hold-Down and Peeling Device: controls the coil head and supports reliable strip threading.
- Entry Pinch and Feeding Unit: grips and advances the strip into the processing line.
- Entry Leveler / Straightening Unit: prepares the strip for stable tracking when required by the material and process.
- Side Guide and Centreline System: aligns the strip precisely before the slitting section.
- High-Precision Slitter Head: carries the circular knives and spacers that divide the master coil into finished strips.
- Knife and Spacer Arrangement: supports the specified slit pattern, strip width and tolerance requirement.
- Scrap Edge Winder: collects trimmed edge scrap in a controlled manner.
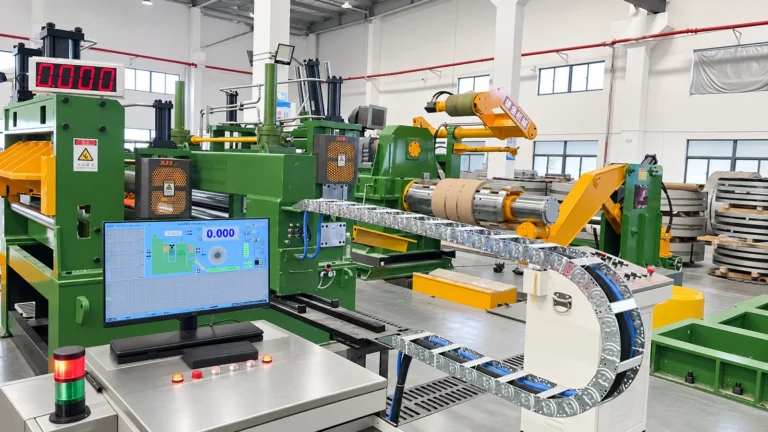
- Belt Tension System: applies stable, adjustable strip tension to support orderly strip separation and coil build.
- Strip Separator and Pre-Separator: keeps slit strips separated before recoiling.
- Recoiler: builds compact finished coils with coordinated tension control.
- Coil Support Arm and Discharge Car: assist finished-coil support, removal and downstream handling.
- PLC/HMI Control System: centralises operating commands, status monitoring and coordinated line control.
- Hydraulic, Pneumatic and Safety System: powers the configured actuators and supports safe operation.
Controlled Recoiling
How the Belt Tension System Supports Coil Quality
The belt tension section is installed between strip separation and recoiling. It applies controlled back tension to the slit strips before they enter the recoiler, helping each strip remain evenly tensioned and correctly guided during winding.
Its synchronised belt contact reduces relative sliding at the strip-contact surface. This is especially valuable for surface-sensitive coil such as stainless steel and pre-painted/color-coated material, where stable strip handling helps reduce the risk of handling marks during recoiling.
Adjustable belt pressure and tension settings are matched to the strip width, thickness, material strength, surface condition and slit pattern. Together with the separator system and recoiler, the belt tension section helps build tight, orderly finished coils, maintain strip spacing, and stabilise exit-side operation during speed changes.
1850 High Precision Slitting Line Gallery
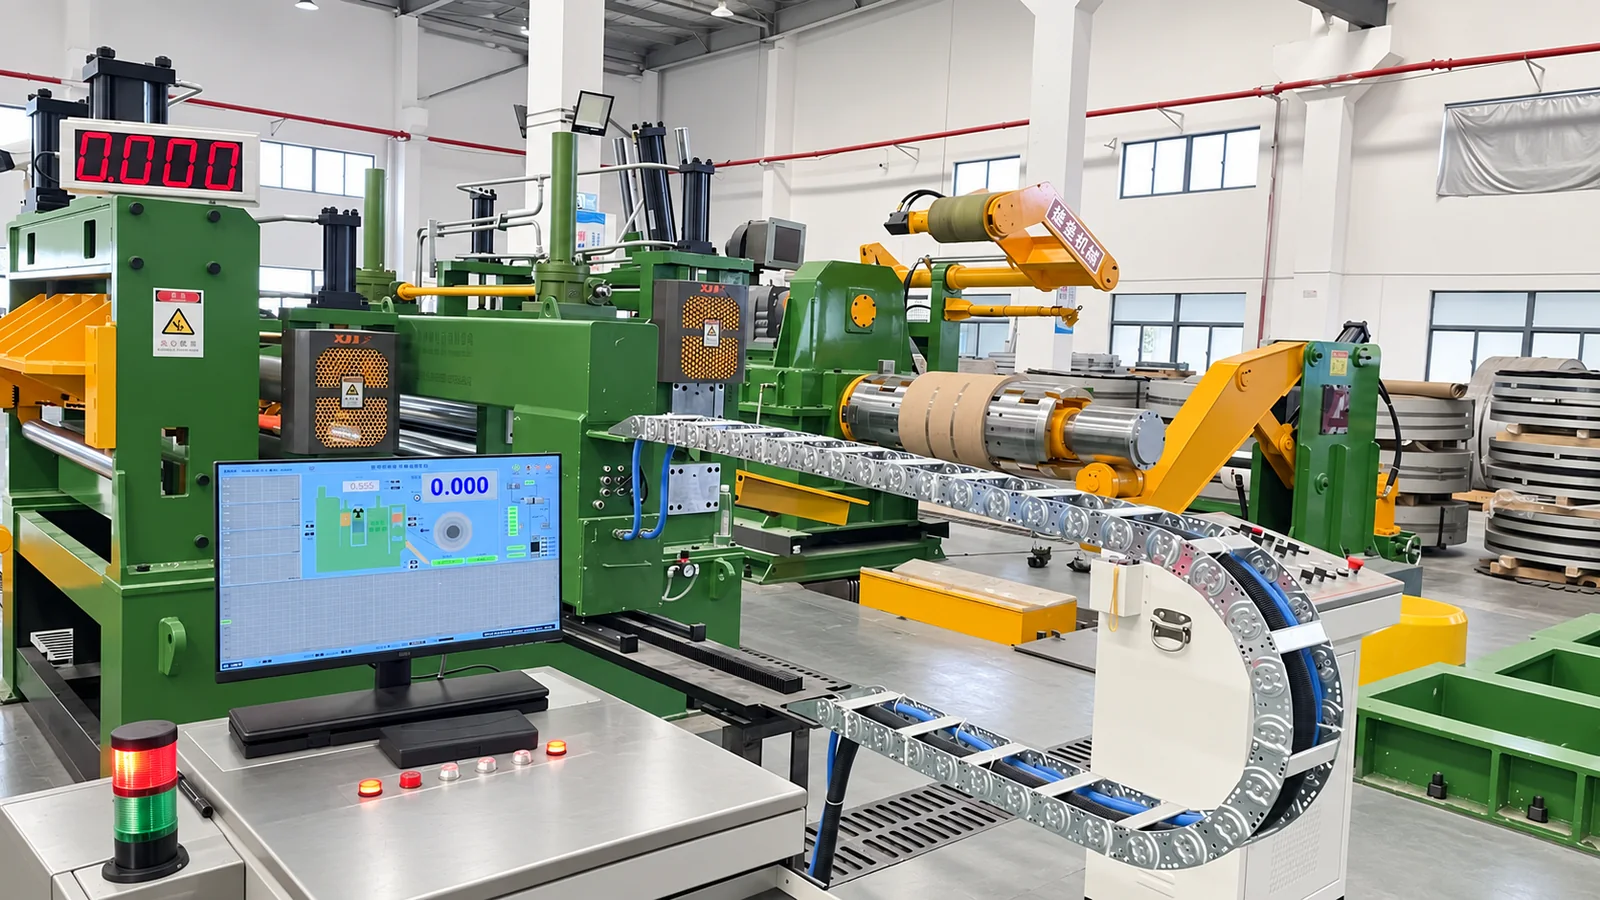
1850 High Precision Slitting Line Process Video
Watch the 1850 high-precision slitting line with belt tension system in operation.
XIONGJIN MACHINERY WORKSHOP — FINISHED PRODUCT
See finished XIONGJIN equipment in the workshop and delivery-ready product area.
More XIONGJIN MACHINERY WORKSHOP Videos
See more XIONGJIN machinery, workshop processes and finished equipment.